Profile extrusion with PolyAl: dies, calibration and line speed
How to dial-in single-screw extrusion lines for decking, fencing and technical profiles using recycled PolyAl pellets.
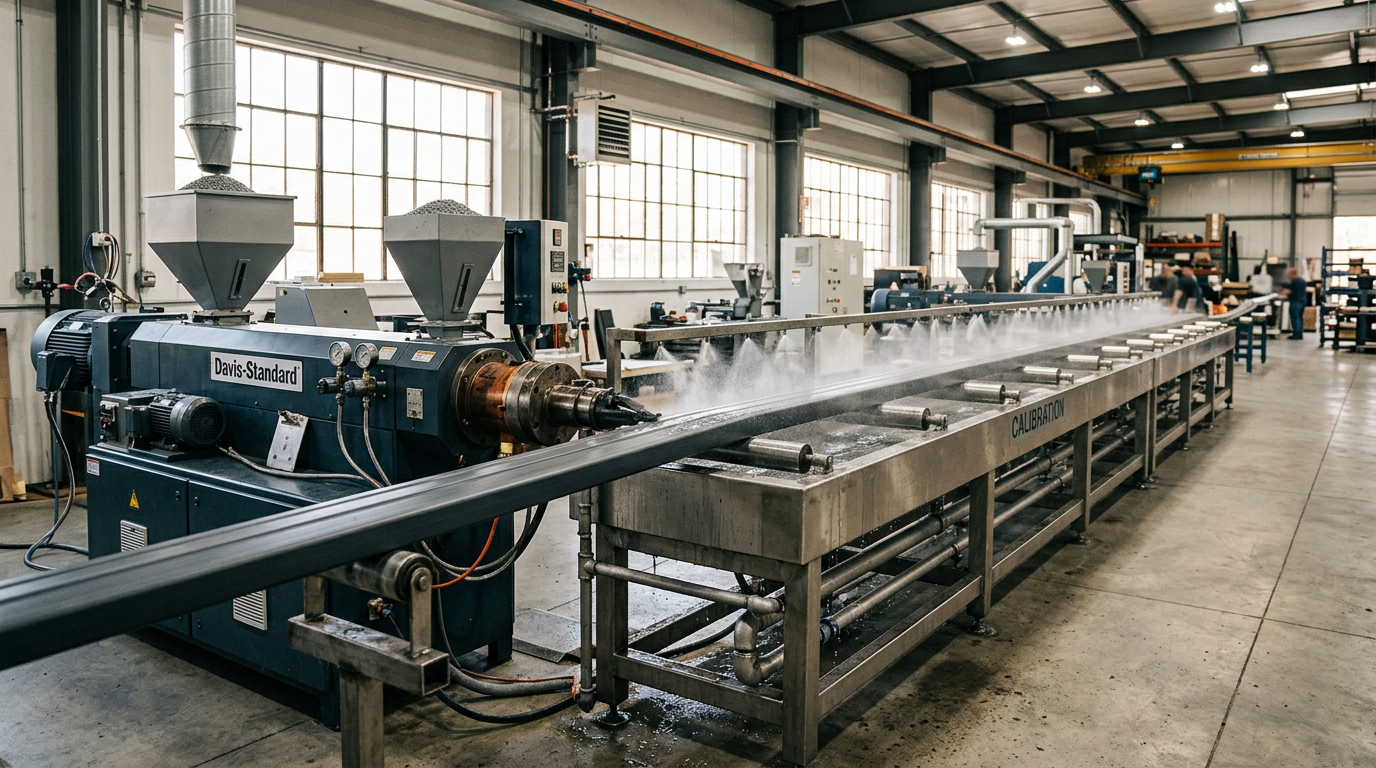
Extrusion is the most common transformation route for PolyAl pellets after pallet injection. The material extrudes cleanly on standard single-screw HDPE lines, but a handful of details matter for first-time users.
Line configuration
- Extruder: single-screw, L/D 28–32, barrier or grooved-feed screw with mixing section, screen pack 60/80/120 mesh.
- Die: flat-die for sheets, profile die for decking/cladding/fencing. Provide generous land length (≥ 10× wall thickness) for dimensional stability.
- Calibration: vacuum calibration table with water cooling. Aluminium-loaded melt cools 10–15 % faster than virgin HDPE — calibrate accordingly.
- Haul-off: caterpillar with cushioned tracks. PolyAl marks more easily than virgin HDPE during the first 2 m after the calibrator.
Temperature profile
For a 90 mm extruder producing a 140 mm decking board:
| Zone | Temperature |
|---|---|
| Feed | 165 °C |
| Compression | 185 °C |
| Metering | 200 °C |
| Adapter | 210 °C |
| Die | 215 °C |
Keep melt below 230 °C. The aluminium fraction radiates heat efficiently — you may run 5–10 °C cooler than equivalent HDPE.
Line speeds
Real-world averages on calibrated lines:
- 140×25 mm decking board: 1.6–2.2 m/min
- 80×40 mm fencing post: 2.8–3.2 m/min
- 40×40 mm cable conduit: 4.5–5.5 m/min
Surface finish
Most decking customers prefer a brushed or embossed finish. PolyAl takes embossing rolls beautifully and the speckled aluminium reads as a premium "stone-like" surface. Co-extrusion with a thin virgin-HDPE cap layer is possible for fully uniform colour.
Tooling wear
Die chrome plating recommended; expect 2–3× the wear of virgin HDPE on screen packs (replace every 800–1200 hours instead of 2000+).
Quality control
- Check density (Archimedes) every 2 h: target 950–1050 kg/m³
- Check dimensional stability after 24 h conditioning
- Tensile test (ISO 527) once per shift on extruded coupon
Bottom line
A mid-range extrusion line that runs HDPE today can produce PolyAl decking and fencing tomorrow with no capital investment beyond a slightly more aggressive screen-pack schedule.